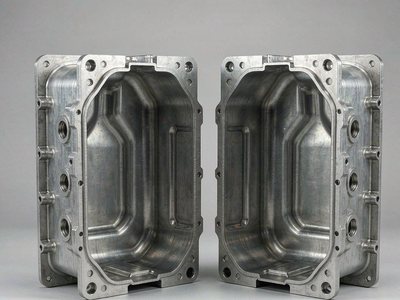
 Extrusion Blow Molds for HDPE Bot
 ABS/PC Electronics Housing Inject
Product Details
Welcome to Taizhou Huangyan Jinting Plastic Mould Co., Ltd. official website!
- Scan for Mobile Store

Mold manufacturing, PET preforms


Price¥680.00
MOQ1 setStock:0 set
 Company Card
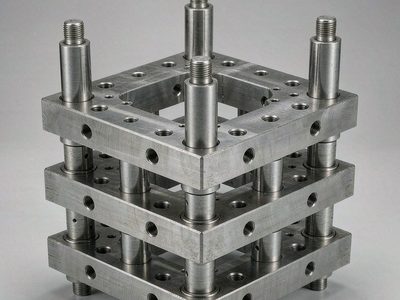
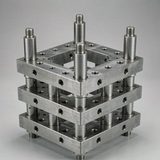
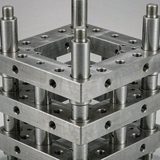
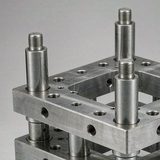
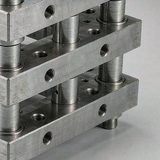
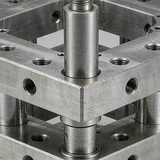
A mould base is the machined steel frame that holds every other component of an injection tool: the cavity and core inserts, the ejector system, the guide pillars and the cooling circuit. Buyers who treat it as a commodity item usually discover the consequences at the trial stage, when plate flatness, pillar alignment or insufficient support causes flash, wear or a tool that cannot hold tolerance after 200,000 shots. This page explains how standard and custom mould bases are specified, and what to inspect before approving a quotation.
A two-plate base is the baseline design. It carries a top clamping plate, cavity plate (A plate), core plate (B plate), support plate, spacer blocks and a bottom clamping plate. Adding an ejector plate set, a stripper plate or a third plate changes the assembly but not the underlying logic: every plate has to be flat, parallel and hard enough to resist wear at the guide and return-pin bores.
Standard bases follow regional systems such as the LKM, Futaba, DME and HASCO patterns. They are stocked in common sizes, which keeps cost and lead time low. Custom bases are machined to a specific insert pocket, undercut or multi-cavity layout, and they are unavoidable once the part geometry falls outside the standard grid.
Plate grade is not the only variable. Thickness tolerance, flatness and the quality of the guide-pillar fit usually separate a base that survives production from one that does not. Ask for the inspection record rather than the material certificate alone.
For matching plate steel to the part application, our guide to injection mold steel selection compares P20, 718H and S136 in production terms. For part geometry that constrains the base design, see the plastic part design guidelines.
Standard bases win on price and availability, and they are the right answer for most tools up to roughly 600 mm × 600 mm with a rectangular insert layout. Custom bases add machining hours and inspection time, but they avoid the compromise of forcing a cavity layout into a stock frame — a compromise that often shows up as uneven cooling or an ejector pattern that marks the part.
The practical rule is to compare total tool cost rather than base cost. A base that is 15% cheaper but needs two extra fitting days and a re-cut pocket is not cheaper. Buyers sourcing tooling in China can review plastic moulds and tooling listings, or check toolmaker credentials through the company directory before releasing a purchase order.
WeChat Support
Mobile Store
