Product Details
Welcome to Xiamen IntiMed Manufacturing Co., Ltd. official website!
- Scan for Mobile Store

TPE molding, private-label kits, plain outer packaging



Price¥0.85
MOQ2000 pieceStock:0 piece
 Company Card
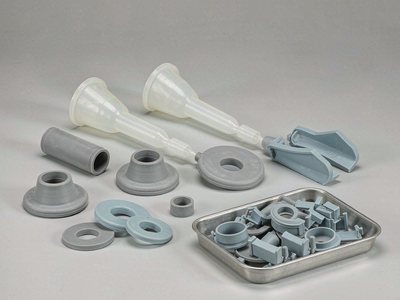 Moulded TPE and Silicone Accessor
¥0.55/piece
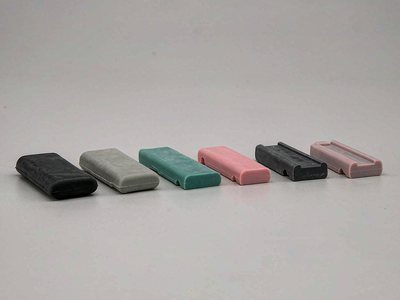 Custom Soft TPE Molding Shore 0-3
¥0.16/piece
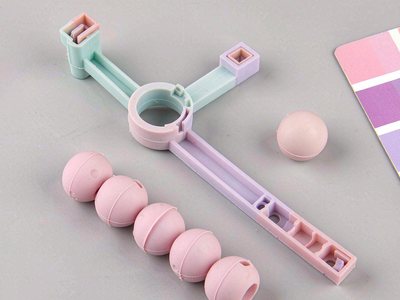 Silicone Ring and Bead Accessory
¥0.08/piece
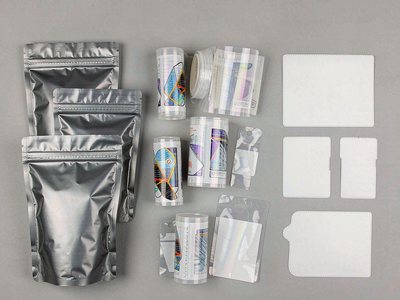 Discreet Polybag and Shrink Sleev
¥0.06/piece
Phthalate Free TPE Overmolding on
¥0.85/piece
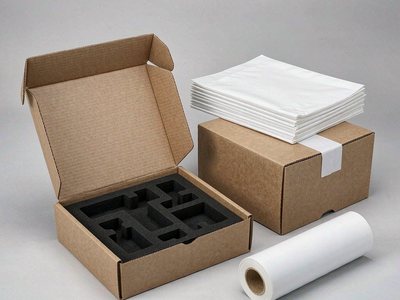 Discreet Neutral Packaging and Mo
¥0.42/piece
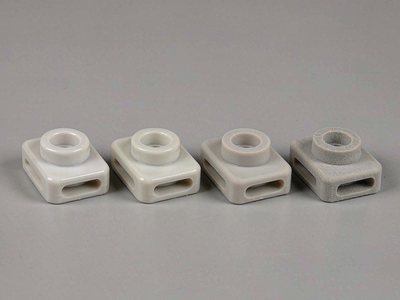 Custom Texture Silicone Novelty M
¥0.22/piece
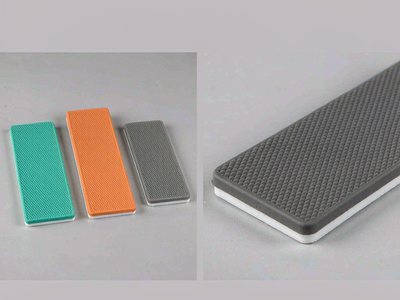 Soft Touch TPE Overmoulded Grip P
¥0.42/piece
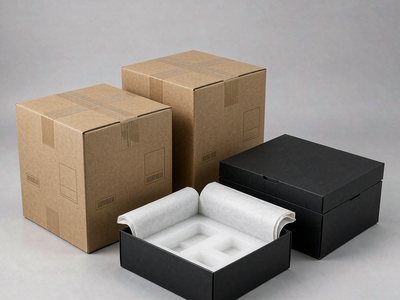 Blind Ship Carton and Rigid Gift
¥0.95/piece
Overmoulding is chosen for one of two reasons: to make a part easier to hold, or to make a rigid part safe against an impact. Both reasons need the elastomer to stay attached, and the attachment is a bond, not an adhesive.
We overmould SEBS-based TPE onto ABS and PC cores in Xiamen, with tooling and colour matching in-house.
TPE on an SEBS base bonds chemically to ABS and PC through the polystyrene-compatible phase in the elastomer, so the bond survives cleaning agents and repeated flexing. Overmoulding onto PP or PE does not bond without a primer or a corona treatment, and where a customer asks for PP we either recommend an ABS core or quote a bonding step as a separate process. A part that peels after six months is almost always a material mismatch rather than a process fault.
| Elastomer | TPE, SEBS base, phthalate and latex free |
|---|---|
| Hardness | Shore 0 to 30 A |
| Cores | ABS, PC, or a supplied metal insert |
| Bond | Chemical, no primer required on ABS and PC |
| Colour | Matched to Pantone, Delta E under 1.5 |
| Surface | Matte, gloss, or soft-touch coating |
| MOQ | 2,000 pieces per SKU |
Overmoulded walls need enough thickness to flow without shorting the cavity, typically 0.8 mm minimum on a 30 A grade and 1.2 mm on a 0 A grade. The transition line between core and elastomer is designed into the tool as a step rather than left to the flow front, because a flow-front transition produces a feather edge that lifts after cleaning. Where the part is gripped, the elastomer is usually ribbed: ribs give grip without increasing the compression force on the core.
Two-shot overmoulding needs a tool with a core-plate index, which costs more than a single-shot tool but removes an assembly step. For volumes under about 5,000 pieces a two-shot tool is usually the wrong answer, and a sequential two-shot on two presses is cheaper. Tooling runs 25 to 35 days, and first articles are checked for bond strength by a pull test on a sample coupon rather than by eye.
Bond is verified by a 90 degree peel test on a sample from each lot, and by an immersion test where the part will be washed. Compression set and tear strength are recorded against the buyer's specification. Any product-level certification is arranged by the buyer.
Material declarations cover phthalates, heavy metals and latex. Where the destination market requires REACH or food contact compliance, documentation is supplied for our material. Copy and imagery are kept to a non-explicit commercial standard.
Tel:
Mobile:
Email:
Address: Haicang District, Xiamen, Fujian, China
WeChat Support
Mobile Store
