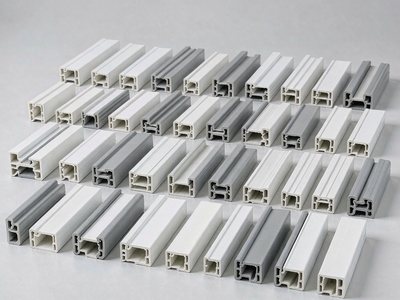
 Co-Extruded Dual Color and Soft-H
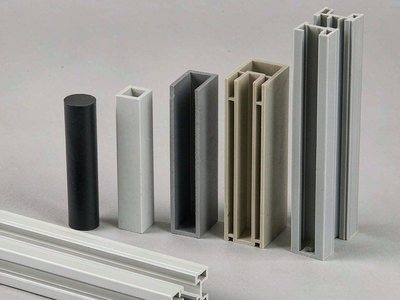 Custom Plastic Extrusion Profiles
 Custom Neck Finish Closure Toolin
 Plastic Bottle Closures Child Res
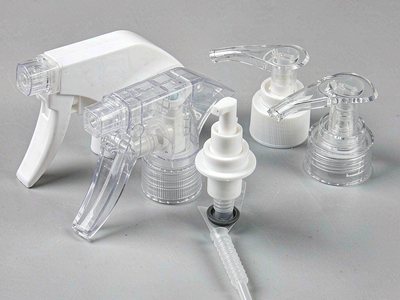 Trigger Sprayer and Lotion Pump F
Product Details
Welcome to Taizhou ClosureTech Packaging Co., Ltd. official website!
- Scan for Mobile Store

High-cavity closure molding, liner insertion, extrusion



Price¥0.22
MOQ1000 pieceStock:0 piece
 Company Card
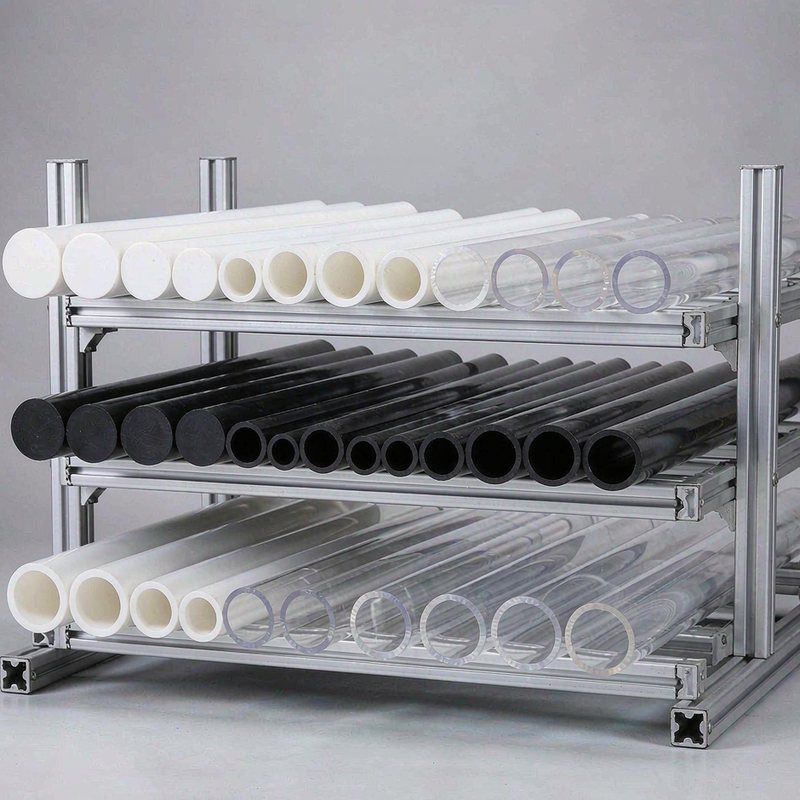
Stock rod and tube look like a commodity purchase until the parts start failing. A roller cover that warps after machining, a bushing that binds because the bore was cut before the stress relaxed, a tank window that crazes at the drilled holes: all three come from the same root, and it is not the extrusion.
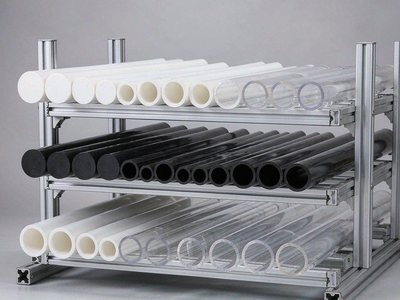
We extrude and supply plastic rod and tube cut to length, with secondary machining performed from annealed stock and a stated tolerance.
Rod and tube are extruded through a die and cooled in a calibration bath, and the tolerance that matters is not the diameter alone but the concentricity: a tube whose wall is thick on one side will not hold a bore and a rod that is slightly oval will run out when turned. Diameter is held to h9 or h11 as the programme requires, and the concentricity is stated in the specification rather than left to the die.
Extruded stock carries residual stress from the die and the cooling. A rod machines true and then relaxes over the following hours, moving out of round or bowing. The fix is annealing: the stock is heated to just below its softening point and cooled slowly, which relaxes the stress before the machining rather than after. Every machined part in this programme is cut from annealed stock, and the annealing is stated in the spec so the buyer knows why the lead time is what it is.
| Materials | PVC, PP, PE, ABS, PC, PMMA, PA |
|---|---|
| Forms | Solid rod, tube, channel bar |
| Diameter tolerance | h9 or h11 as quoted |
| Cut length tolerance | plus/minus 0.5 mm |
| Machining | Drilling, milling, turning, from annealed stock |
| Surface | As extruded or machined finish |
| MOQ | 1,000 pieces or 500 kg per material |
Roller covers and idler rollers turned from PP or ABS, bushings and spacers from PA or POM, tank and vessel windows from PC or PMMA, and pump and valve bodies machined from PVC bar where a moulded body would need a tool the volume does not justify. The machined-from-stock route is the right answer for dozens to a few thousand pieces and the wrong answer above that, which is why the quote states the volume at which a moulded part becomes the cheaper option.
Cut-to-length is quoted with the tolerance stated, because a tube cut on a chop saw splinters at the exit face and a tube cut on a latere-cut or a fine-tooth saw with support does not. Bundles are capped so the cut ends do not chip in transit, and the pack is sized to the diameter: a bundle of 25 mm rod travels fine, a bundle of 100 mm rod needs end caps and a rigid carton or the ends arrive chipped.
The honest answer at quotation: machined parts from stock are cheaper up to roughly 2,000 to 5,000 pieces depending on the part, and more expensive above it, because the stock cost is paid on every piece and the machining is paid on every piece. Where a programme is growing, the quote includes a moulded alternative with the tool amortised, so the buyer can see the crossover rather than discovering it at reorder.
Our custom extrusion profile programme covers the profile angle, and the extruded profiles and rods category lists the full range.
Tel:
Mobile:
Email:
Address: Huangyan District, Taizhou, Zhejiang, China
WeChat Support
Mobile Store
