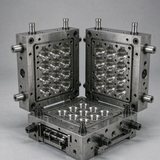
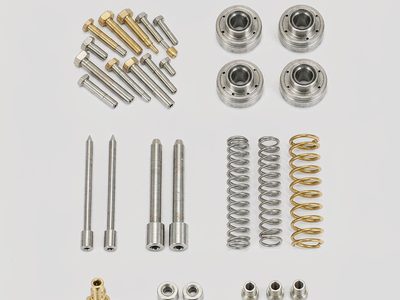


Every injection mould eventually consumes parts. Core pins retract and return a million times, guide bushes wear, and sprue bushings erode where abrasive fillers pass. When one component fails, a productive tool becomes scrap — and the difference between a one-day fix and a three-week stoppage is whether the replacement can be sourced quickly and correctly. This page covers the standard components inside an injection mould, the specifications that decide interchangeability, and how buyers source plastic injection mold parts without gambling on a line.
The Components Inside an Injection Mould
- Ejection system — ejector pins, sleeves and stepped pins, the parts that see the highest cycle counts and earliest wear.
- Guide system — guide pillars and guide bushes that keep the two mould halves aligned shot after shot.
- Feed system — sprue bushings and locating rings that take the nozzle's abuse and locate the mould on the platen.
- Sliders and lifters — angle pins, wear plates and heel blocks for undercuts and side actions.
- Cooling components — baffles, bubbler tubes and plugs that direct water through the core and cavity.
Standards and Interchangeability
Most standard components follow catalogued systems — DME in North America, HASCO in Europe and MISUMI across Asia — so a replacement pin from any conforming supplier drops into the same bore. The trap is the mixed tool: a mould assembled with one system's bushings and another's pins will run, then bind. When sourcing, the standard must be read off the tool drawing or the existing part, not assumed from the mould's country of origin. Custom components — contoured ejectors, core pins for a specific rib profile — have no standard, so those parts live or die on the drawing.
Material and Specification Points
- Material — SKD61 (H13-type) for most pins and bushings; SKH51 high-speed steel where wear resistance dominates; powder-metallurgy grades for glass-filled resins.
- Hardness — typically 50-62 HRC for pins, matched to the surrounding block hardness to avoid differential wear.
- Tolerance — pin diameters ground to h6 or better, with length tolerances tight enough that the flush setting survives regrinding.
- Coatings — TiN or TiAlN on ejector pins where lubricant is limited; coatings change fit, so the bore allowance must be agreed in advance.
- Surface finish — a controlled polish, because a rough pin galling in its bore means a full teardown.
Sourcing Plastic Injection Mold Parts Without Gambling
Ask for the material certificate and a hardness reading rather than a marking on the box, and confirm the standard system explicitly. For high-volume lines, keep a spare set of the highest-wear components — ejector pins, guide bushes, sprue bushings — on the shelf, because a mould waiting on a ground pin is a press earning nothing. A supplier who can reverse-engineer a worn part and confirm fit before shipping is worth more than the cheapest quotation.
Standard and custom mould components sit under plastic moulds, while moulding partners able to fit and test replacements are listed under custom molding services. The mold design gate types guide covers how feed geometry drives wear, and the supplier directory supports factory-level screening.