
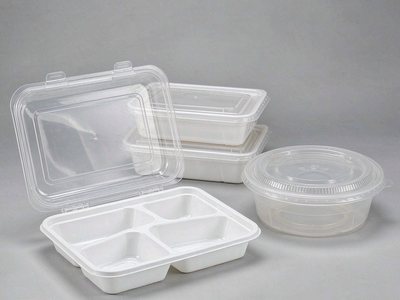

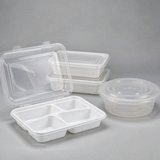
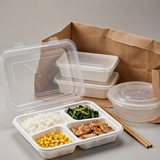
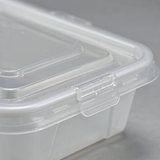

A plastic lunch box manufacturer sits at the meeting point of food safety, retail presentation and daily abuse. The container is microwaved, washed, stacked, dropped and sealed hundreds of times, and it has to keep its shape and its closure through all of it. Buyers who select on appearance alone usually discover the failure modes later: hinge cracking, seal loss after dishwashing, or warping that stops the lid seating.
Material Choice Sets the Ceiling
PP is the default for reusable lunch boxes because it tolerates microwave reheating and dishwasher cycles without deforming. PS and PET give better clarity for cold-display packs but are not suitable for hot fill or microwave use. Anything claiming microwave safety should state the maximum temperature and the test basis, not just a symbol on the artwork.
Food-contact compliance is a separate question from heat resistance. For the US market the reference is FDA 21 CFR 177, for the EU it is Regulation 10/2011 with a declaration of compliance per material. Our walk-through of FDA food contact compliance sets out what that documentation should contain.
Structure: Where Most Complaints Originate
- Single compartment vs divided — dividers add stiffness but create thin walls that cool unevenly and warp. Position matters more than count.
- Seal design — a silicone gasket in a moulded groove holds better than a flat lip against flat lip, especially after washing.
- Vent valve — needed if the box will be microwaved closed; without it the lid lifts or the seal inverts.
- Hinge — living hinges need the right PP grade and a defined flex direction; separate pin hinges cost more to assemble but survive more cycles.
- Stacking — a recessed lid that accepts the base of the box above saves retail shelf space and shipping volume.
Customisation and Minimum Order
Colour and printing are the usual customisation points, and both carry minimums tied to the mould and the printing method. In-mould labelling gives a fully decorated wall with no label edge, but needs a dedicated tool. Pad printing and heat transfer are cheaper to start and easier to change between orders.
Send the intended use, the number of reheating cycles expected, the closure type and the destination market's food-contact requirement. That is enough for a plastic products supplier to recommend a mould family and quote realistically. Buyers comparing several container formats should also look at the wider manufacturer base before locking a tool, since a shared mould family often shortens lead time more than a price negotiation does.
