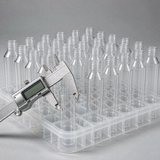
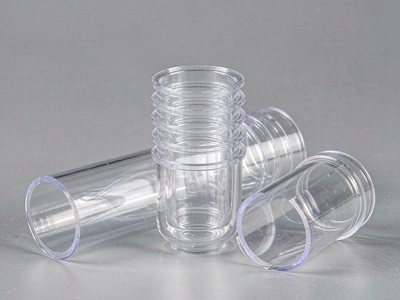

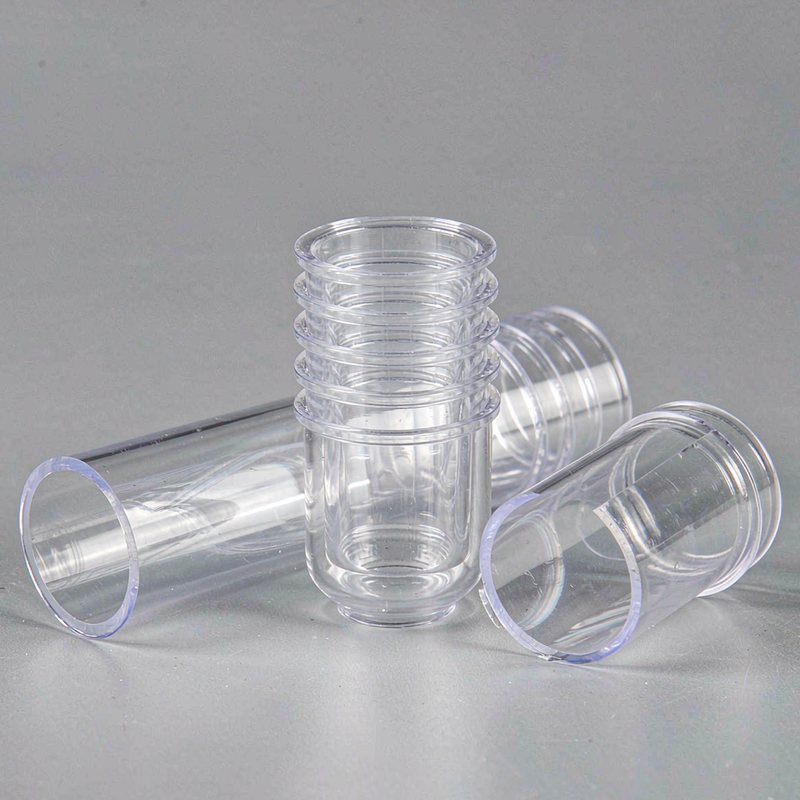

A preform is a short, thick-walled PET tube with the finished bottle neck already moulded into it. We injection mould preforms that our customers then stretch blow into finished bottles. Selling preforms rather than bottles lets packaging buyers run their own blow moulding line, or ship a standard preform into several markets and blow locally.
Why the neck is moulded, not blown
The neck carries the thread and the tamper-evident bead, and both need a dimensional accuracy that blow moulding cannot deliver. Moulding the neck in the injection stage and then only stretching the body means the closure fit is defined by the tool steel, not by process drift in the blow moulder. A 24/410 preform will take any 24/410 closure on the market, so the buyer can change cap supplier without changing preform.
Construction
- Injection moulded in one shot into a hot-runner tool, no cold runner regrind
- Neck with moulded thread and anti-backoff slots
- Base section formed as a hemispherical or petaloid blank for uniform wall distribution after stretch
- Intrinsic viscosity controlled to 0.78 to 0.84 dl/g, dried to below 50 ppm before moulding
Specification
| Neck finish | 24/410 SP400, 28/410, 38/410, PCO1881 on request |
|---|---|
| Preform weight | 8.5 g (200 ml) to 48 g (2.5 L) |
| Barrier option | Standard PET, or multilayer with nylon or EVOH |
| Colour | Clear natural, or custom with masterbatch batch certification |
| Packing | Bagged in tubes, 1,050 pcs per carton |
| MOQ | 50,000 pieces per neck finish |
Wall distribution is the whole job
A preform is not a simple tube. The wall thickness varies along its length so that, after stretching, the bottle wall is uniform. Get the preform profile wrong and the blow moulder will produce a bottle that is thin at one point and thick at another, and the thin point becomes the burst failure or the creep failure on a hot-fill line. We run a wall-thickness map on every new preform and supply the data with the tool handover.
What we need from you
The finished bottle drawing, the fill volume, the closure specification and the filling line's blow moulder model. That last one matters: preform geometry has to match the stretch ratios of the specific blow moulder, and a preform tuned for a Sidel machine will not perform identically on a Krones. If you are still selecting equipment, we can supply a generic preform and a stretch test report.
Certification
Food-contact grades are supplied with EU 10/2011 and FDA statements, and a certificate of analysis per lot covering IV, acetaldehyde and colour. For hot-fill applications we can also supply a heat-set compatible grade.