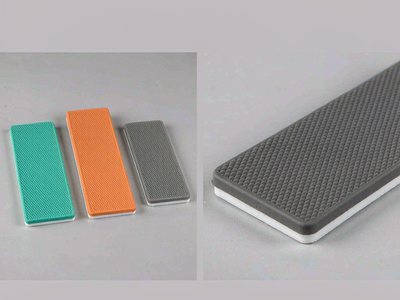

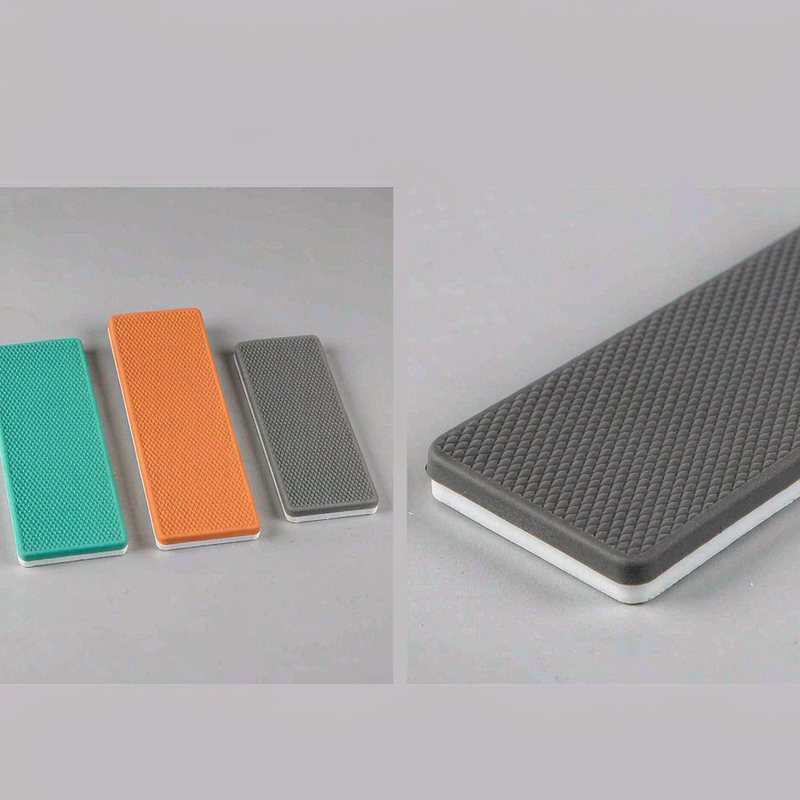

A grip panel is the most-touched part on any handheld product and the first part to show wear. Grips that turn shiny and slick after a season, or that separate at the edges after a drop, trace back to two moulding decisions: the compound shore and the mechanical lock between the two shots.
We mould two-shot grip panels for power tools, kitchen appliances and handheld device brands, with the TPE shot onto a rigid core in a single tool or a rotating two-shot tool.
Why the lock matters more than the adhesive
TPE bonds chemically to most rigid cores, but a chemical bond alone is not a design. The lock is mechanical: the core carries undercut grooves, through-holes or a dovetail profile so the TPE has to tear to separate. A grip that relies on adhesion fails at the first impact, because the impact load arrives at the edge where the bond is weakest. A grip with a mechanical lock fails only if the TPE itself tears, which at Shore A 55 to 70 is a load the user cannot generate.
Hardness for sweaty hands
Soft compounds feel premium on a shelf and turn slick in use. For a tool that will be gripped hard and used warm, the working band is Shore A 55 to 70 with a matte, textured surface: firm enough to transmit force, textured enough to drain sweat. Hot-climate programmes are quoted at the harder end with a coarser texture, because texture does more for retention in wet conditions than softness does.
Texture options
- Diamond knurl. The tool-grip standard; moulds cleanly and wears well.
- Rib pattern. Directional grip for rotation-heavy tools; moulds with a slight draft-friendly ridge.
- Fine matte. Appliance panels; hides fingerprints and scuffing, less retention.
Specification
| Core | PA6, PA66, ABS or PC, glass-filled option |
|---|---|
| Overmould | TPE, Shore A 55 to 70, phthalate-free declared |
| Lock | Undercut grooves and through-holes per drawing |
| Texture | Diamond knurl, rib or fine matte |
| Adhesion | Peel test per first article, break mode reported |
| Colour | Pantone or RAL matched, delta-E tolerance quoted |
| MOQ | 5,000 pieces per colourway |
Two-shot routes and what they cost
The rotating-tool route moulds the core, rotates the tool and shoots the TPE on the same press: the parts stay warm, the adhesion is best, and the tool is the most expensive. The two-press route moulds the core on one press and transfers to a second press for the overmould: cheaper tooling, but the core must be re-heated or the bond is compromised. Small panels usually justify the rotating tool; large appliance panels, where the tool cost dominates, often run the two-press route with a documented re-heat window.
Adhesion verification
Every first article batch is peel-tested: the TPE is cut free at one edge and pulled at a defined rate. The result is reported as a break mode, not just a force, because a cohesive break inside the TPE proves the bond held, while an adhesive break at the interface means the core was moulded with release agent carried over from a previous job. Where a core material changes mid-programme, adhesion is re-verified, because the same TPE bonds differently to ABS than to glass-filled PA.
Wear, UV and chemical resistance
Tool grips see sunscreen, oil and solvent wipes. TPE resists most of them, but plasticiser-free does not mean stain-proof, and dark dyes in sunscreen mark light compounds first. Where the programme is sold in the same channel as outdoor equipment, UV stabilisation is quoted for the TPE as well as the core, because an unstabilised TPE surface cracks before the core degrades.
Production notes
Cycle time runs 35 to 50 seconds depending on panel size and grip wall. The core shot is sequenced first and the overmould second, with the core still warm enough for adhesion but cool enough to hold the insert. Where a programme runs several grip colours on the same core, the core is moulded in one colour and the grip carries the colour variable, which keeps colour-change scrap to the TPE alone.
Related reading
Our phthalate free TPE overmolding programme covers the generic core angle, and the TPE and TPR intimate products category lists the full range.