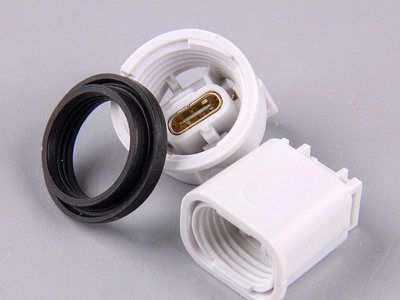

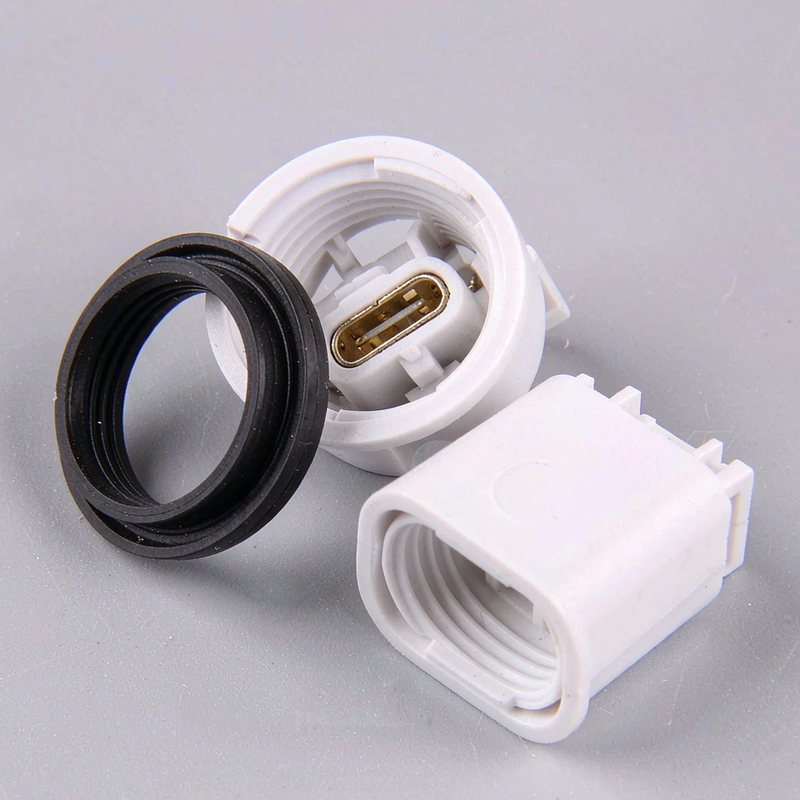

On a rechargeable device, the charging port is where water gets in and where the cable pulls out. Both failure modes concentrate at the same interface, and both are solved in the tool: the connector is placed in the mould and the housing is shot around it, so the seal and the retention are moulded features rather than assembled ones.
We insert-mould USB-C charging ports for rechargeable wellness, personal care and small appliance programmes, with overmoulded seals and per-batch verification.
Why insert-moulded rather than assembled
An assembled port sits in a pocket and is held by friction or an adhesive, and the pocket is where water tracks. An insert-moulded port is captured by the plastic itself: the housing is shot around the connector body, so there is no gap to track along and no adhesive to degrade. The trade is tool complexity, because the connector has to be held square in the tool while the plastic flows around it at 250 to 280 C.
Holding the connector in the tool
The connector is placed on pins or a nest in the tool and held by a spring-loaded clamp. Three problems follow. The clamp must not flash over the mating face of the connector, because a burr there makes the cable seat badly. The shot must fill around the connector shell without short-shot at the root, which needs a gate positioned to flow around rather than into the nest. And the part must cool without pulling the connector out of square, because a port that sits a fraction off-angle wears the cable.
The seal
An IPX7 port seal is a compressed ring, either an O-ring placed in the tool or a gasket shot in a second operation. The O-ring route is more reliable because the compression is set by the groove, not by the cycle; the second-shot gasket route is cheaper and needs a groove depth controlled to a tenth. Where the device is only splash-rated, a moulded tongue that covers the port is enough, and the programme is quoted with the rating stated as a design target rather than a promise.
Specification
| Connector | USB-C, 6-pin or 16-pin, gold-plated contacts |
|---|---|
| Housing | ABS, PC or PC/ABS shot around the connector |
| Seal | Overmoulded O-ring, groove-controlled compression |
| Retention | Pull test per first article, force and break mode reported |
| Insulation | Dielectric check per batch |
| Colour | Natural, black or Pantone matched |
| MOQ | 3,000 pieces per connector and colourway |
Verification per batch
- Connector retention: cable pull to the quoted force, break mode reported
- Seating check with a gauge plug: the cable inserts without force and holds
- Insulation resistance across the pins at the quoted voltage
- Flash inspection at the mating face under magnification
Plating and corrosion
Ports fail in the field more often from corroded contacts than from anything the moulding did. Gold plating thickness on the contact is specified by the connector supplier, and the moulder's contribution is handling: connectors are kept sealed until the insert step, and the finished ports are packed with a dust cap or a protective plug. A programme that ships devices with open ports should expect contact corrosion complaints regardless of the plating.
Strain relief
The cable fails at the port entry long before the port fails. The usual answer is a moulded strain-relief boot overmoulded onto the first few millimetres of cable, which spreads the bend radius over the boot instead of concentrating it at the connector. Where the boot is a separate part, it is quoted with the port so the two are approved together; a boot that slips on the cable is a boot that was moulded without a mechanical groove.
Production notes
Connector loading is the labour content of the operation, done by a pick-and-place with vision verification rather than by hand at volume, because a connector placed off-square passes a visual check and fails the retention test in the first article. Cycle time runs 25 to 40 seconds, and the insert loading step is quoted separately from the shot so the labour is visible in the price.
Related reading
Our IPX7 massager housing programme covers the device-level enclosure, and the personal massagers category lists the full range.